

Plenty of warehouse floors look fine on the day the coating cures. Then, six months later, blisters show up near the dock door and the turning lanes start to wear through. The cause is rarely the resin. Usually someone picked the product by color, price or a compressive strength figure, and nobody checked the slab or the traffic first.
Choosing industrial epoxy flooring comes down to five questions. Can the slab take a coating? How much moisture is in it? What rolls over it every day? What chemicals and temperatures hit it? How many hours can the site actually shut down? Settle those, then pick primer, body coat, texture and topcoat as one matched system.
Below, we turn those site conditions into a specification you can hand to a supplier, for warehouses, factories and workshops.
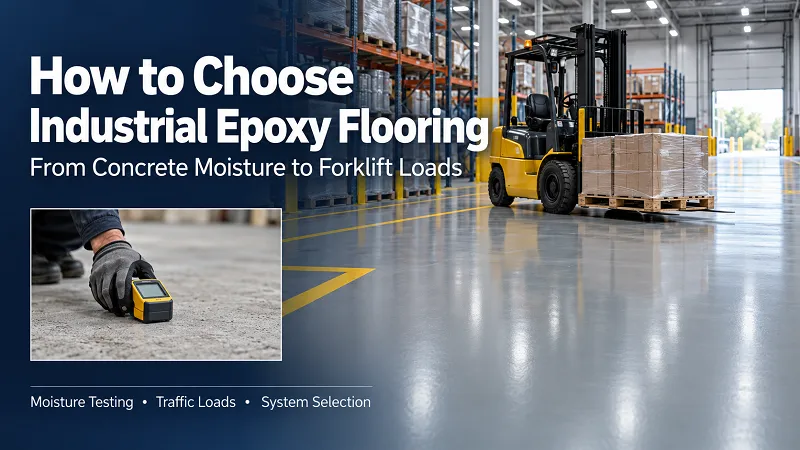
1. Inspect the Concrete First
Walk the floor with the person who runs the building. Mark cracks, broken joint edges, oil stains, hollow-sounding patches and spots where water pools. Ask whether a coating has peeled here before — and whether it peeled in the same places.
A 28-day-old slab isn’t automatically ready for epoxy. Cure age and moisture readiness are two separate things. How fast a slab dries depends on its thickness, the air around it, and whether moisture has a way out.
Older slabs are a different job. Oil soaks well below what you can see. Weak laitance or badly bonded patch material will undermine any new coating on top. Grinding off the surface layer doesn’t always remove deep contamination.
So write the preparation into the spec: mechanical profiling to the level the chosen system requires, repairs, and where it makes sense, a trial patch with pull-off adhesion testing. A strong resin on weak concrete still fails.
2. Know What Your Moisture Test Actually Measures
“Moisture below 4%” means little until someone names the test method. A reading from an electronic meter, an internal relative humidity figure and a vapor emission rate are three different measurements. None converts into another.
ASTM F2170 uses in-situ probes to measure relative humidity inside the slab. ASTM F1869 uses anhydrous calcium chloride on bare concrete to measure vapor emission, in pounds per 1,000 sq ft over 24 hours. Different questions, different answers. [1, 2]
Handheld meters earn their keep for mapping — they show where the wet areas are. Use one for acceptance only if the flooring manufacturer names the instrument, the procedure and the allowed reading. And log where and when you tested, instead of trusting one number taken by the door.
No single moisture limit fits every epoxy floor coating. Some systems need fairly dry concrete. Others include a moisture-control layer with its own acceptance criteria. Compare your results against the written limits for the whole proposed system.
Then find the source. Leftover construction water, a missing vapor retarder, a leaking pipe and groundwater pressure each call for a different fix. “Moisture-tolerant” on a primer label does not mean it is a vapor barrier. If mitigation is needed, use a documented, compatible assembly — and stop any active leak before installation starts.
3. Look Past the Forklift’s Rated Capacity
A “three-ton forklift” is a lifting rating. It isn’t the weight on your floor. The truck itself, its battery or fuel, the driver and the payload all add up, and wheel loads shift with load position and truck layout.
Ask the equipment maker for loaded axle or wheel-load data. Note tire material, wheel size, trips per day, braking zones and turning points. Hard wheels with small contact patches concentrate stress. Tight turns add shear at the coating surface.
Docks, aisle intersections and chipped joint edges usually see harsher service than a straight lane. Don’t overlook pallet jacks either — small, hard wheels can beat up a joint even when the total load is far below a forklift’s.
Compressive strength alone predicts very little here. What matters is abrasion resistance, impact resistance, adhesion, system thickness and the condition of the substrate. Compare lab results only when the test methods and conditions match.
One more point: the slab carries the vehicles and racking. An epoxy topping protects the surface — it doesn’t add meaningful structural capacity. If you’re unsure about the slab, get an engineer to check it, especially under heavy equipment and rack baseplates.
4. Match the System to Each Zone
Don’t put one build over the whole building just because you want one color. A storage room, a main forklift aisle and a loading bay can each need something different.
The ranges below are starting points for discussion. They aren’t forklift ratings or universal requirements, so confirm final thickness and suitability with your supplier.
| System | Indicative thickness | Starting point for selection |
|---|---|---|
| Thin film epoxy coating | Below 1 mm | Dust control and lighter service on sound concrete |
| Self smoothing epoxy | Around 2–3 mm | Dry production areas and suitable warehouse traffic |
| Aggregate broadcast epoxy | Often around 2–4 mm | Textured surfaces and areas needing added traction |
| Epoxy mortar or screed | Around 4–6 mm or more | Demanding wear, impact, or suitable surface rebuilding |
One product-specific example: Flowcrete describes a 2–3 mm self-smoothing epoxy for dry areas with rubber-wheeled forklift traffic. That doesn’t make every epoxy at that thickness equivalent. Formulation, preparation and operating conditions still decide. [3]
Check what a quoted thickness covers. Does it include primer and topcoat, or only the body layer? Is it nominal, or the minimum specified build? Put repairs, leveling and moisture mitigation on separate lines so every quote covers the same scope.
5. Check Chemicals and Temperature Together
“Chemical resistant” needs a definition. A maintenance shop deals with lubricants, hydraulic fluid and cleaners. A production line might see acids, solvents or hot process liquids. Each one needs its own assessment.
List the chemical, its concentration, liquid temperature, contact time and cleanup routine. A quick splash and constant immersion are not the same exposure. Ask for resistance data on the finished system you’re proposing, including any limits on staining, softening or loss of performance.
Aggressive exposure may justify a specialist epoxy formulation. But if the floor takes frequent hot washdowns and thermal cycling, put polyurethane cement on the comparison list next to epoxy. Manufacturers make those systems for thermal-shock conditions. [4]
Temperature counts during installation too. Check substrate and air temperature, humidity and dew point against the data sheet. Condensation on the slab can ruin adhesion even when internal moisture readings look fine.
6. Balance Slip Resistance and Cleanability
Smooth epoxy cleans easily, but oil, water and fine dust change its grip. Let those conditions guide the finish for each zone.
Aggregate broadcast systems add texture. The trade-off is that rougher surfaces need better cleaning equipment, and heavy texture traps dirt and slows scrubbing. Too little texture is a problem wherever spills are expected.
Test a sample with real footwear, real contaminants and your actual cleaning method. If a slip-resistance criterion applies, name the test method and the service condition. A dry result says nothing about wet or oily floors.
Plan the transitions as well. Walkways, ramps, production areas and forklift routes may each need a different finish — just avoid abrupt changes that cause cleaning or movement problems.
7. Treat Joints and Cracks as Part of the System
Many early failures start at the joints, not in the middle of a bay. One chipped edge becomes an impact point every time a wheel crosses it.
Work out which cracks are stable and which still move. Specify proper repairs for damaged edges, and detail movement joints so they keep working. Filling every joint with rigid epoxy and coating over it just passes the movement into the finish.
Drains, door thresholds, machine bases and terminations belong in the drawings or the written scope. They affect durability and upkeep, and they’re easy to miss in a price-per-square-meter quote.
8. Plan Downtime Around Full Service Conditions
“Walkable tomorrow” is not “ready for loaded forklifts tomorrow.” Data sheets often give separate times for foot traffic, light mechanical load, full mechanical service and chemical exposure.
Build the shutdown around the return-to-service time that applies, at your real site temperature. Count preparation, repairs, moisture treatment, recoat windows and cure. A cold slab can stretch the schedule a lot.
Fast-cure products can shorten downtime in the right applications, but the whole assembly has to support the promised reopening date. Check compatibility, application conditions and cure requirements — not just the topcoat.
Set up temporary traffic routes and protect finished areas. Letting vehicles on early can damage a floor before it has reached the properties you chose it for.
9. Compare Full Specifications and Lifetime Cost
A low material price says little about the installed floor. Preparation, repairs, moisture control, labor, shutdown and later maintenance can easily outweigh the gap between two resin prices.
Before you ask for quotes, put together a short project brief:
- Floor area, slab age, existing finish, and photos of defects
- Moisture results, with test methods, locations and dates
- Loaded wheel or axle data, wheel type and daily traffic pattern
- Chemical exposures, cleaning temperatures and drainage conditions
- Required texture, appearance and any separate ESD requirements
- Available shutdown time and the conditions for reopening
Then ask every supplier for the full layer sequence, preparation standard, repair scope, thickness, consumption and exclusions. Request current technical data sheets and a maintenance plan. For OEM or private-label supply, confirm that the resin, hardener, aggregates and application instructions all describe the same tested system.
Dividing the floor into proper service zones often gives better value than laying the thickest system everywhere. Put the money where turning, impact, contamination and downtime make a failure most expensive.
Frequently Asked Questions
What concrete moisture level is acceptable for epoxy flooring?
It depends on the test method and on the system you choose. Follow the manufacturer’s written limits. A meter percentage, internal relative humidity and vapor emission rate can’t be swapped for one another.
How thick should epoxy flooring be for forklifts?
Capacity alone doesn’t set a thickness. Look at loaded wheel forces, tire type, traffic frequency, turning, impact and the state of the concrete, then choose a manufacturer-approved system.
Can epoxy flooring go over an existing coating?
Sometimes — if the old finish is sound, compatible and properly prepared. Test adhesion and check for contamination first. Loose or poorly bonded coating has to come off; covering it just passes its weakness to the new floor.
Is a thicker epoxy floor always better?
Extra thickness helps in the right systems. It won’t fix moisture trouble, weak concrete, poor preparation or the wrong chemical resistance. The full specification decides whether the spend makes sense.
Choose the Floor Around the Work It Must Do
Start with the concrete, record the real operating conditions, and select each layer to match. For industrial epoxy flooring, that approach beats picking a product from a strength figure or a “heavy-duty” label.
Planning a warehouse or factory floor? Send Jinhua Resin your floor area, substrate condition, moisture test results, traffic details and shutdown window. We’ll talk through suitable epoxy floor coating options and send product documentation for your evaluation.